Our Commitment to Quality
consistent, compliant and, uncompromising
Delivering Excellence, Every Step of the Way
Quality is at the core of everything we do, it’s a value that’s embedded into our company culture. From raw material sourcing to final inspection, our commitment to quality drives product performance, customer satisfaction, and industry leadership.
We provide complete traceability across every stage of production. Backed by our ISO 9001:2015-certified quality management system, this ensures full transparency and confidence in every order.
We understand that our customers rely on us to protect the integrity of their products and with them their reputation in a competitive environment. Whether for global transit or long term storage, we exceed industry standards to deliver packaging solutions that are consistent, compliant, and uncompromising.
ISO 9001:2015
Certified to Perform
We have operated under recognized quality standards since 1990 to ensure consistency, reliability, and sustainability in every product.
ISO 9001:2015 is our most recent internationally recognised certified standard that outlines the requirements for a robust quality management system (QMS). It signifies an organizations commitment to quality, performance enhancement, and consistently meeting customer expectations.
Custom Packaging Solutions for Various Industries
We understand that every application has unique challenges, which is why we offer tailored consultation services to develop customized aluminum barrier foil solutions. Our expert team works closely with customers to assess their specific storage, transportation, and protection needs—designing custom-sized, shaped, and sealed barrier packaging for maximum protection and efficiency.
Exceeding Industry Standards
Our commitment to quality means you receive industry-leading protection and peace of mind every time. With our ISO 9001:2015 certification, we ensure exceptional quality, reliability, and environmental responsibility.
Our aluminum barrier foil bags are certified to military, anti-static, and food contact standards, offering clean, long-term protection without the need for additional stabilizers or preservatives.
Trusted by Industry Leaders
With over 600 years of combined industry experience, our team supports businesses of every size. Our customers operate in highly regulated, high-stakes industries where failure is not an option.
Industries we support with quality-led packaging:
NO LIMITATIONS ON SIZE, SHAPE OR, QUANTITY
Protect Your Products with the Industry’s Most Trusted Barrier Packaging Solution
Contact our expert team today for a customized solution tailored to your specific packaging, storage, and transportation needs
MilitaryStandards
Our laminate materials are listed in the
US Department of Defense Qualified Products Database
and are compliant with:
- MIL-PRF 131L Class 1
- MIL-PRF 81705F
- DEF STAN 81-147
- NF H 00310
- DIN 55 531
Continuous Improvement,
Consistent Results
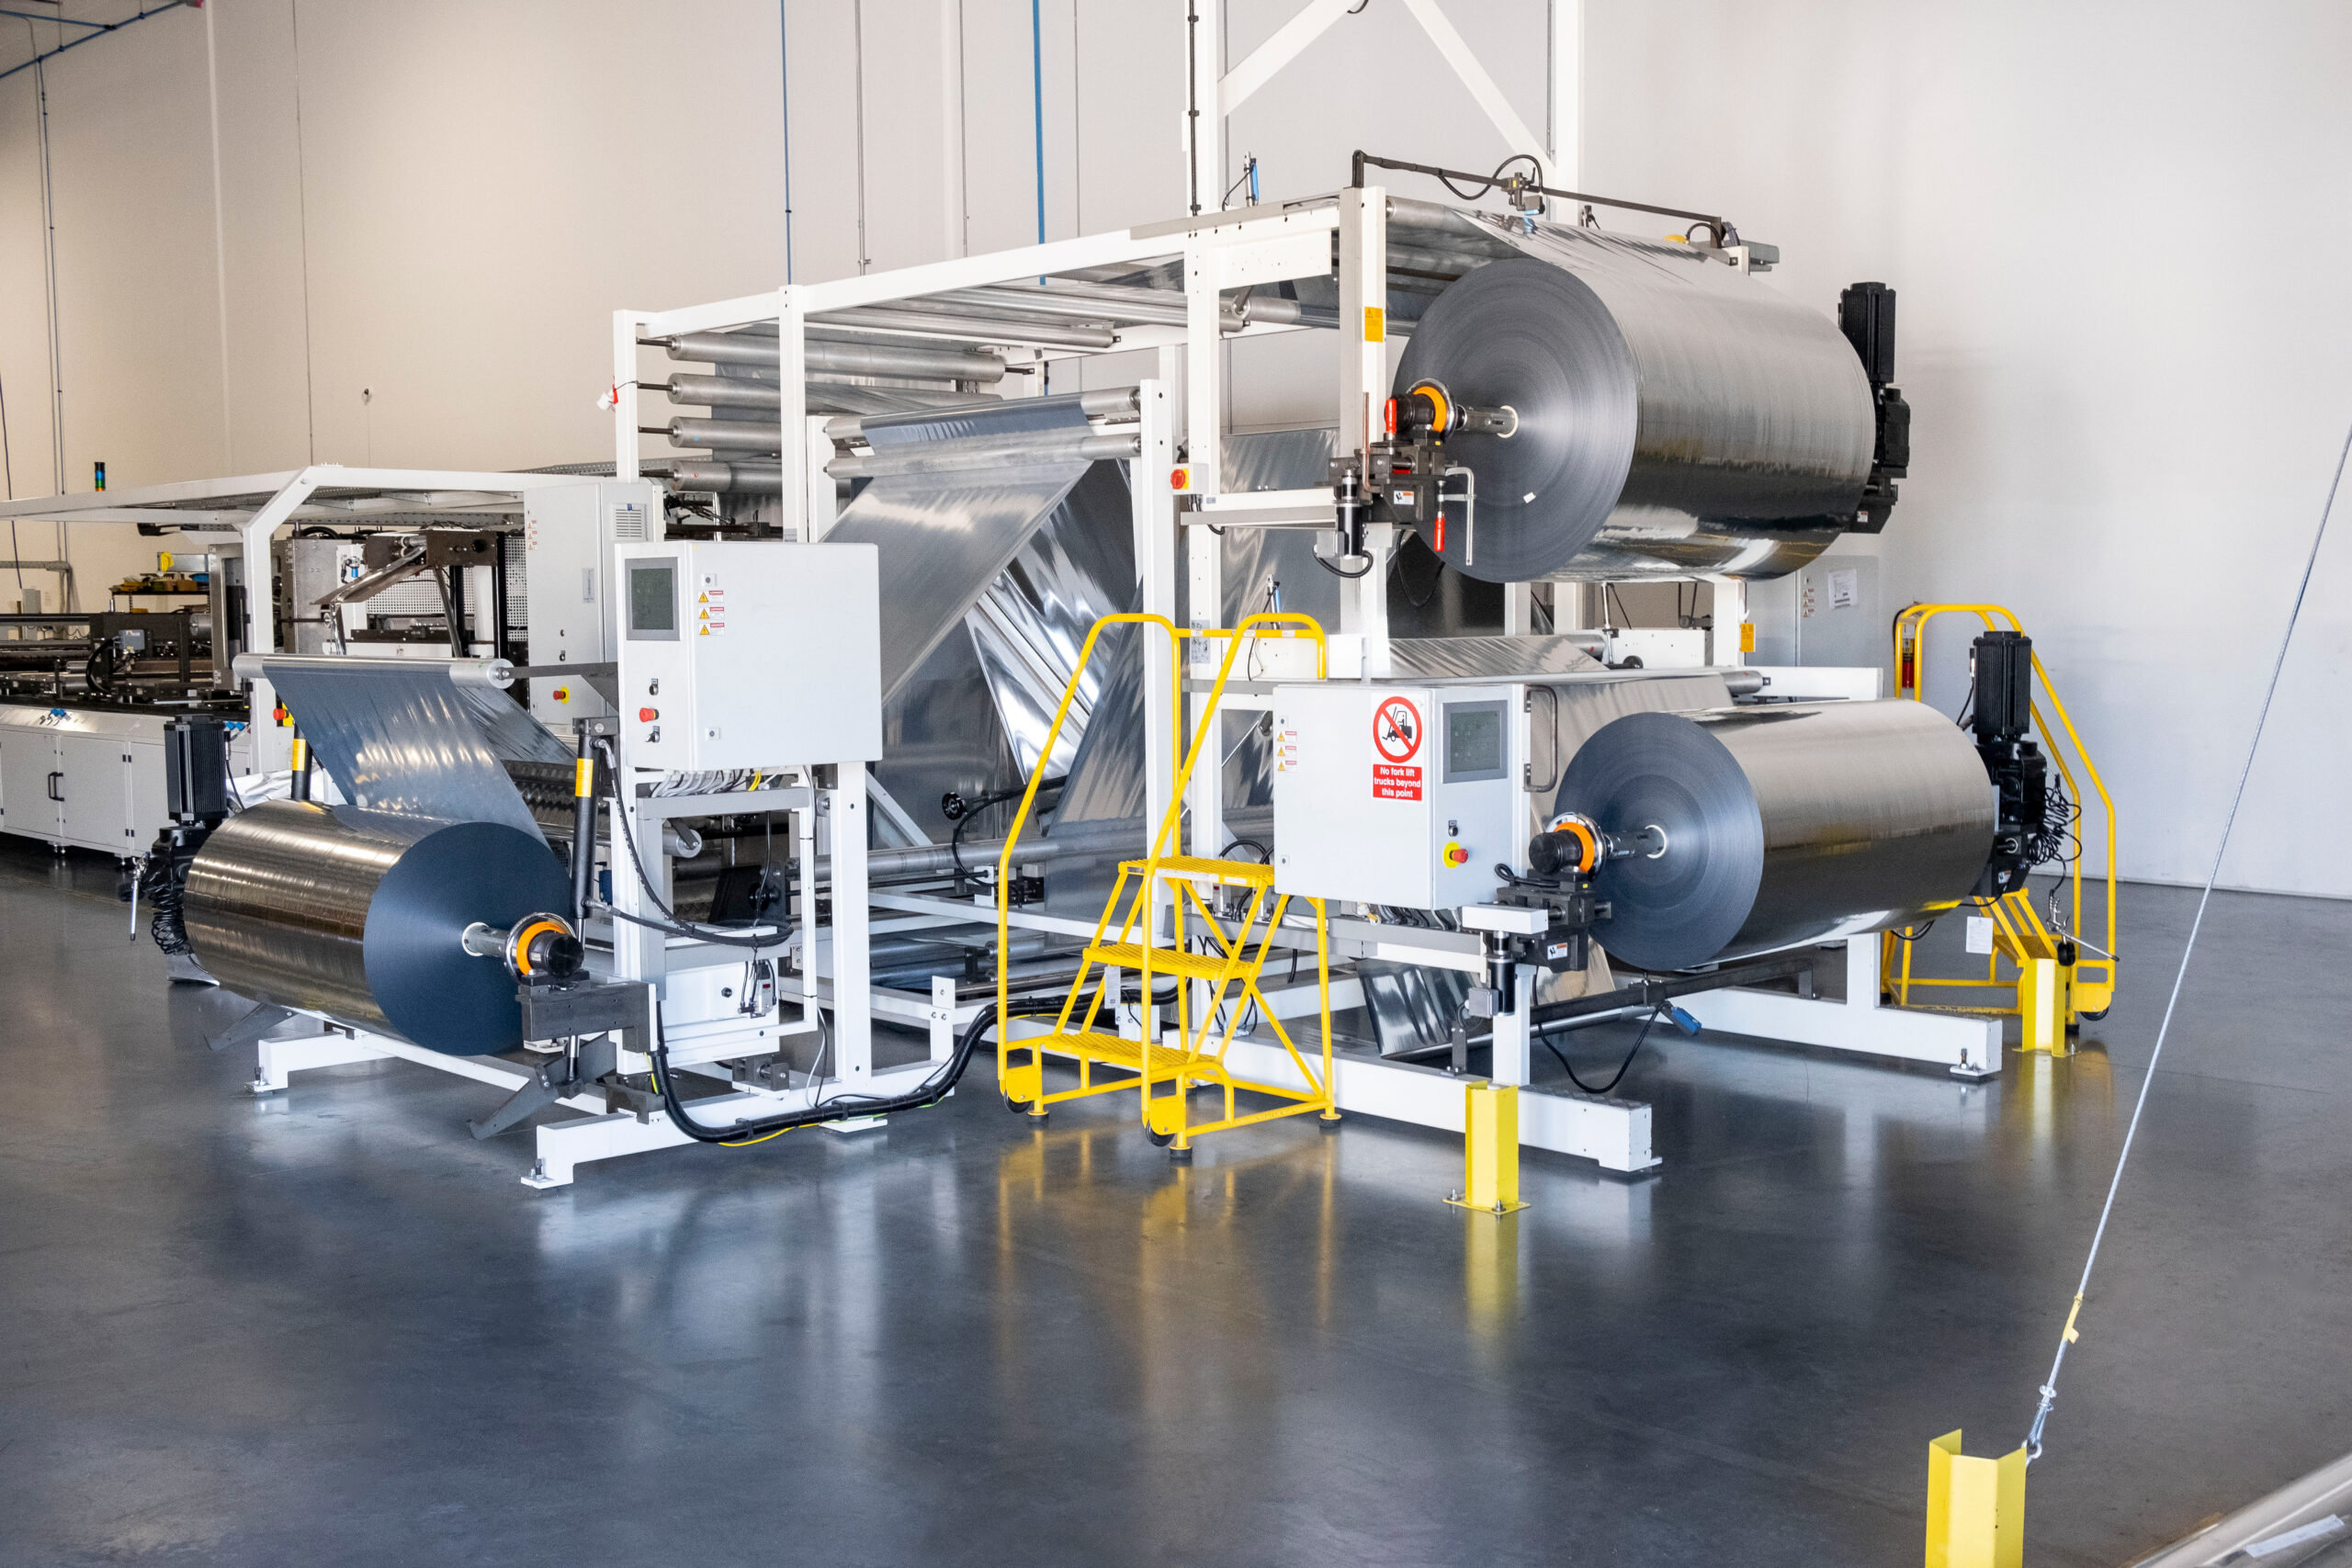
Our commitment to quality embraces operational excellence and continuous improvement of our products and processes. We deliver exceptional quality with repeatable results, driven to achieve zero defect tolerance with efficiency and reliability. Our continuous improvement model applies the concepts of Kaizen, Lean Manufacturing, and Disciplined Problem Solving methods to optimize performance and to ensure every customer receives a packaging solution tailored to the demands and requirements of their product and supply chain. Trial production and approval sampling are available as part of our expert consultation process.
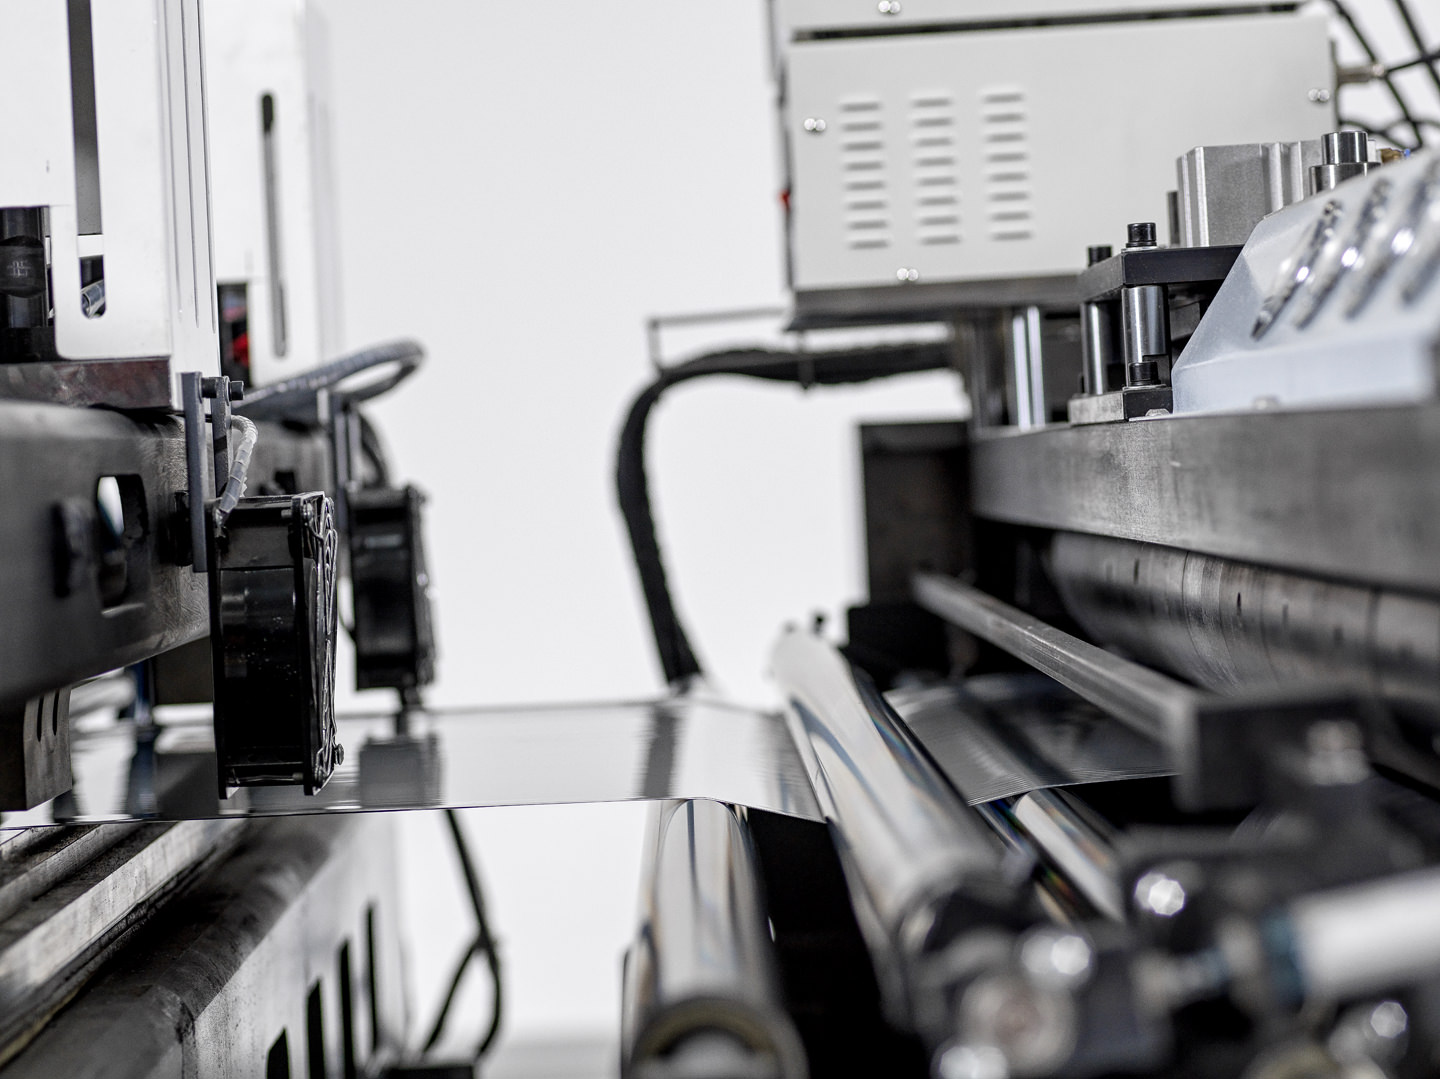
Material And Manufacturing Excellence
All our aluminum barrier foil packaging is made from high-performance, multi-layer laminates, engineered to meet specific mechanical, climatic, and regulatory demands. Whether you require FDA-compliant films, military-grade durability, or static-dissipative properties, we offer:
- Custom laminate structure development
- On-site laboratory testing of materials and prototypes
- Strict in-process quality controls and final inspections
- Hand and automated fabrication under tightly monitored conditions
- Enhanced custom quality measures available as required
Why Quality Matters
- Prevents contamination, corrosion, and moisture damage
- Preserves product integrity and shelf life
- Ensures regulatory compliance across multiple sectors
- Reduces rejection rates, product loss, and returns
- Supports your reputation with reliable, high-performance packaging
Quality That Speaks for Itself
From first contact to final delivery, we are committed to helping your business succeed by preserving product quality. Our mission is simple: craft innovative, high-quality packaging solutions tailored to your needs, preserving product integrity and extending shelf life to ensure your products reach customers in perfect condition, every time.
Related Information
QPD-Listed MIL-PRF-81705 Anti-Static Material: Certified Compliance & Proven Reliability
We’re thrilled to announce that our MIL-PRF-81705 anti-static packaging material has achieved the prestigious QPD-listed certification. This marks our fourth QPD-listed material [link to “Leading The Way” blog], a testament to our
Protecting PUR Hot Melt Adhesives From Moisture Damage
The Challenge Polyurethane Reactive (PUR) hot melt adhesives are a crucial adhesive in various industries, including automotive, packaging, construction, and electronics. They provide strong, flexible, and long-lasting bonds that are ideal for applications
A Guide To Our Custom Barrier Foil Mil-Spec Packaging
Why Is Mil-Spec Packaging Important? Mil-spec packaging is essential in the supply chain because it ensures that military items are protected and can withstand harsh climatic conditions during transportation and storage, thereby guaranteeing
A Quick Look Inside 3D Barrier Bags Inc.
Who is 3D Barrier Bags Inc? Now with over 35 years of industry experience, we have established ourselves as a global leader in climatic packaging solutions. We specialize in protecting dried products and
Packaging Powerhouses: How Our Chandler Facility is Elevating Arizona’s Industrial Supply Chain
Opened in 2024, our new packaging plant in Chandler strengthens our capacity to meet growing demand in the Western U.S., while offering faster lead times and creating local jobs. Chandler Industrial Packaging Solutions
Built for Reliability: Why U.S. Assembled Packaging Matters More Than Ever
Every Bag Made Domestically For You In today’s fast-moving markets, consistency and reliability are everything. But when you’re sourcing packaging from across the globe, things don’t always go as planned. Shipping delays and