Follow us on LinkedIn

Aluminum Barrier Foil Solutions for

Chemicals Packaging

24 HR LEAD TIMES
NO MINIMUM ORDER QUANTITY
OUTSTANDING QUALITY
CUSTOM SOLUTIONS

Why Choose Our Chemical Packaging Solutions?

Keep Your Chemicals Safe from Production to Delivery

Designed to shield against moisture vapor, oxygen, temperature fluctuations and contaminants, our aluminum barrier foil packaging preserves chemical stability, prevents contamination and extends product shelf life.

Secure Shipping and Handling

Our bags and liners provide essential protection for safe transport, handling and storage, especially when working with sensitive or hazardous chemicals.

Compatible with Gas Flushing

To prevent chemicals from reacting with gases in the air during filling, our barrier foil can withstand gas flushing, which forms a temporary dry atmosphere.

RELATED PRODUCTS

Chemicals packaging: Comprehensive protection

POWDERED & SPECIALTY CHEMICALS

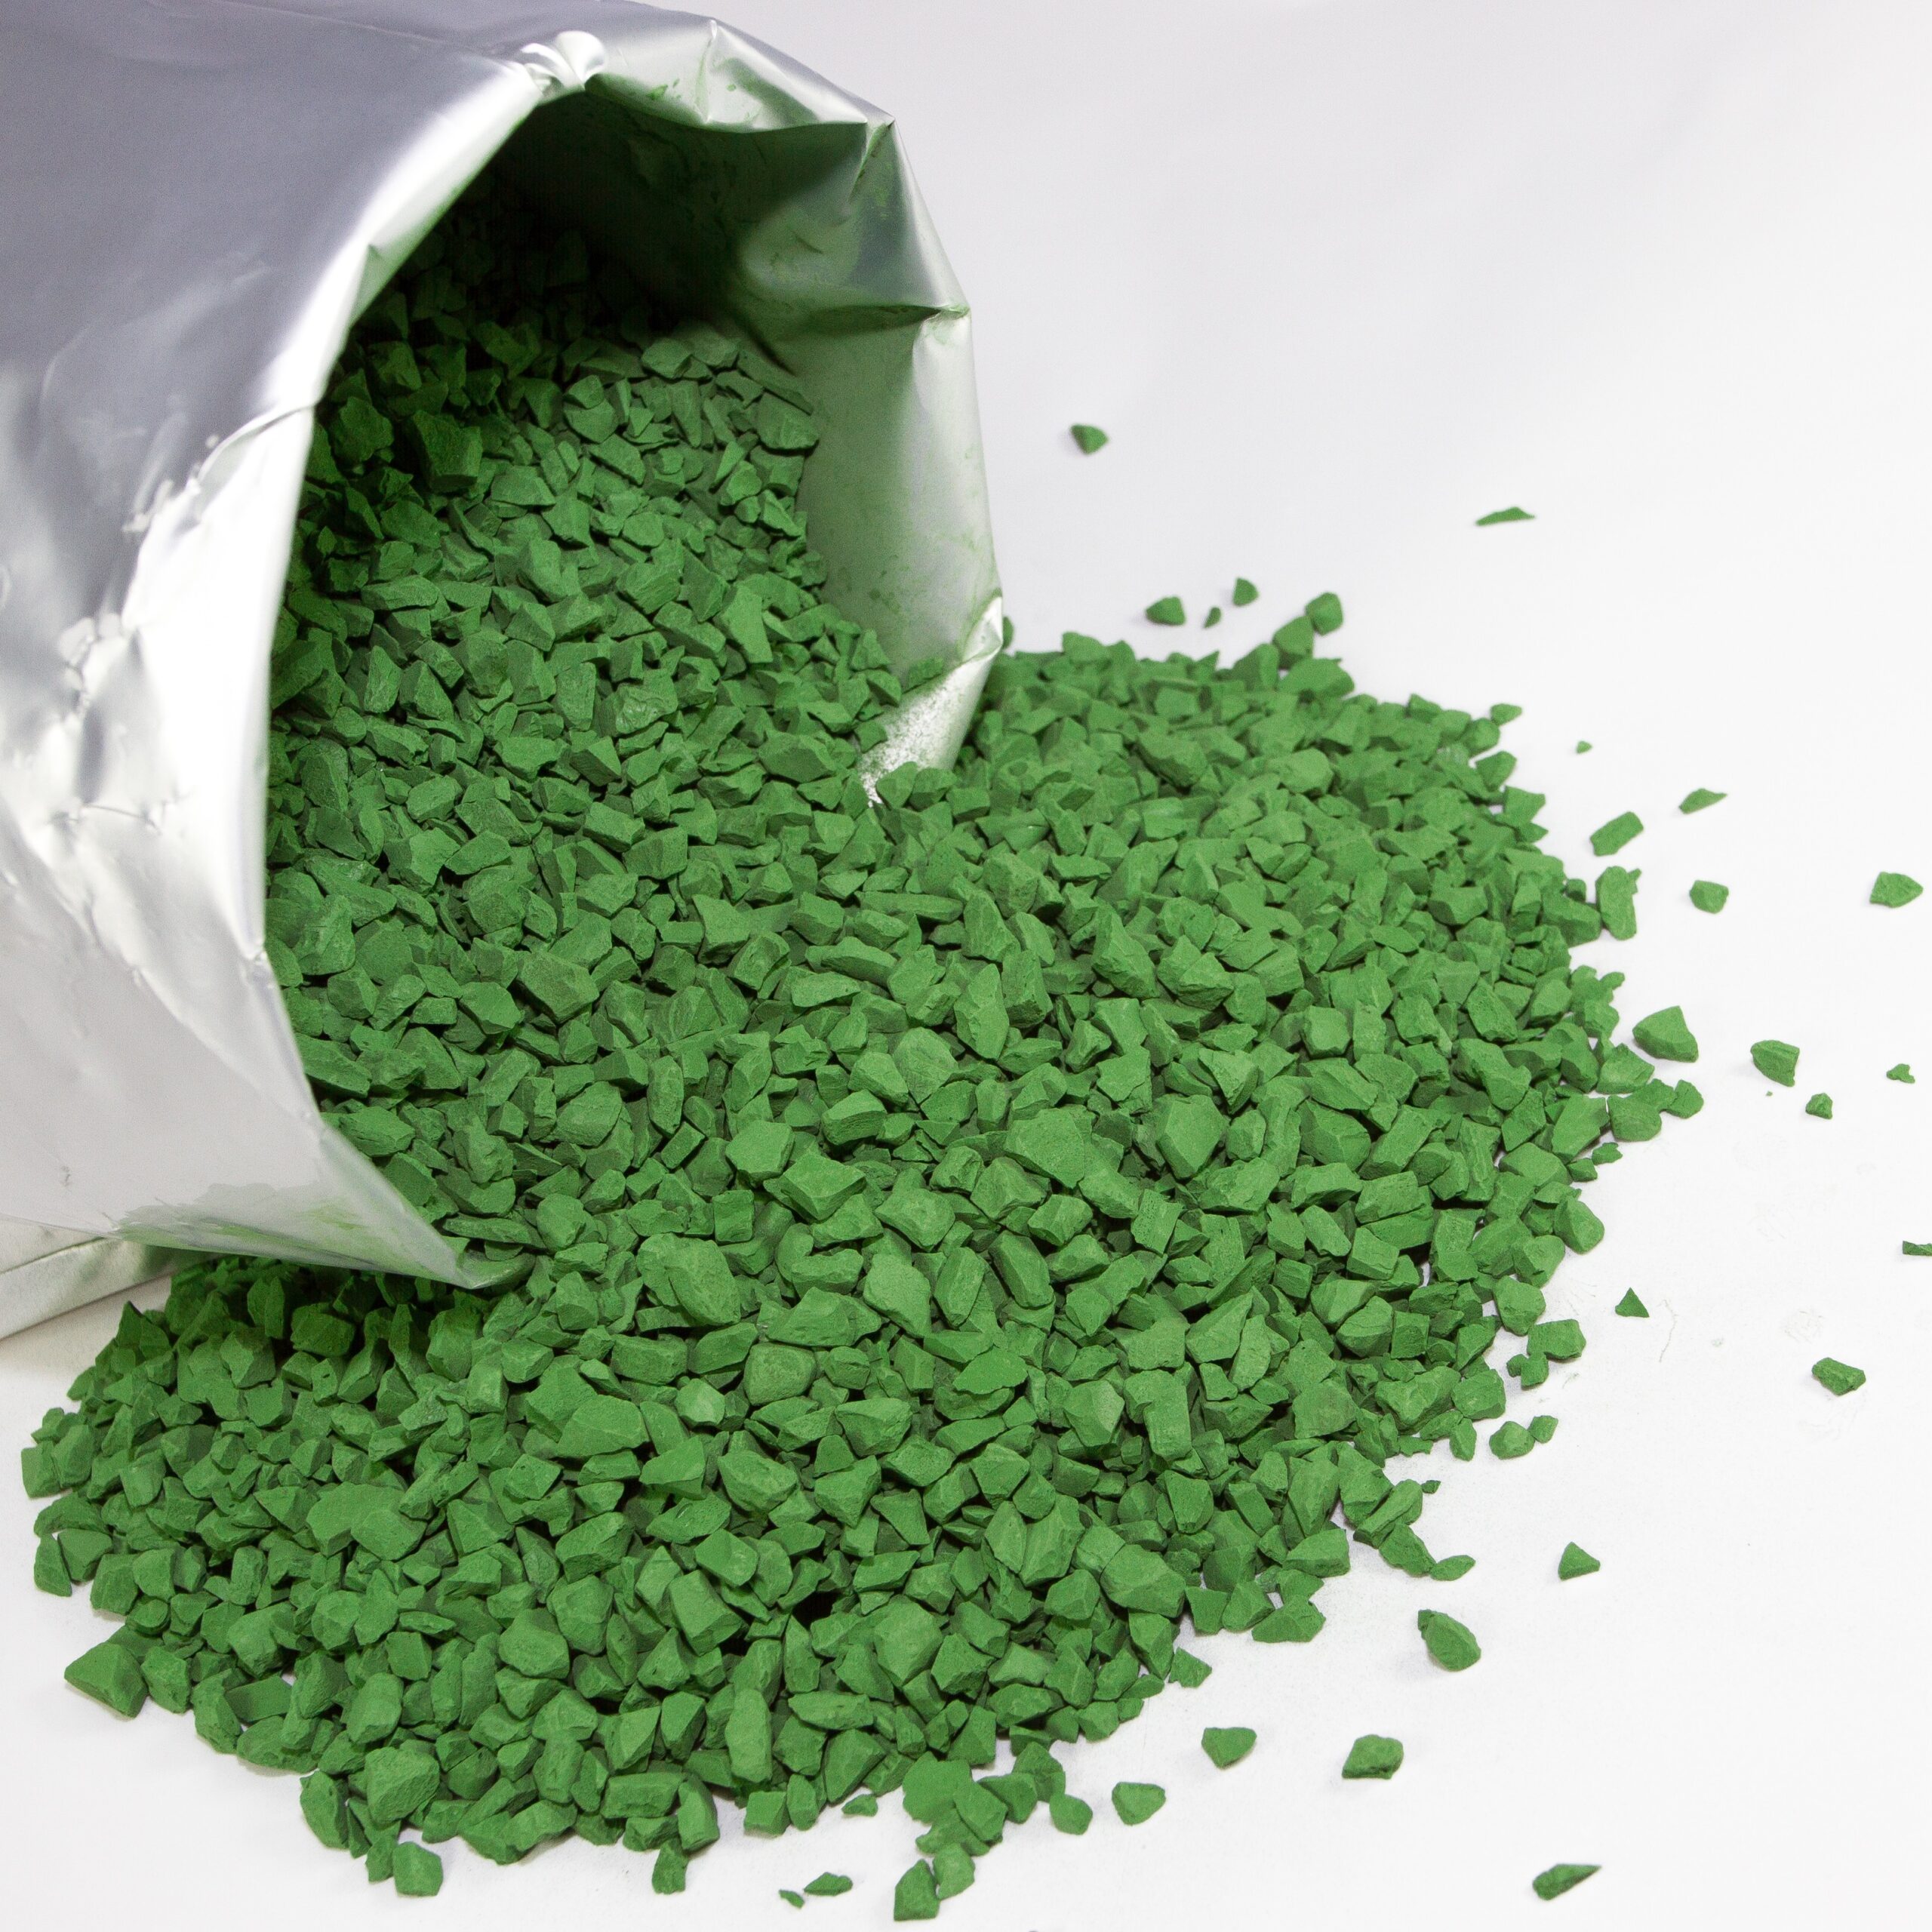
Prevents moisture absorption, caking and degradation, ensuring consistent composition and performance.
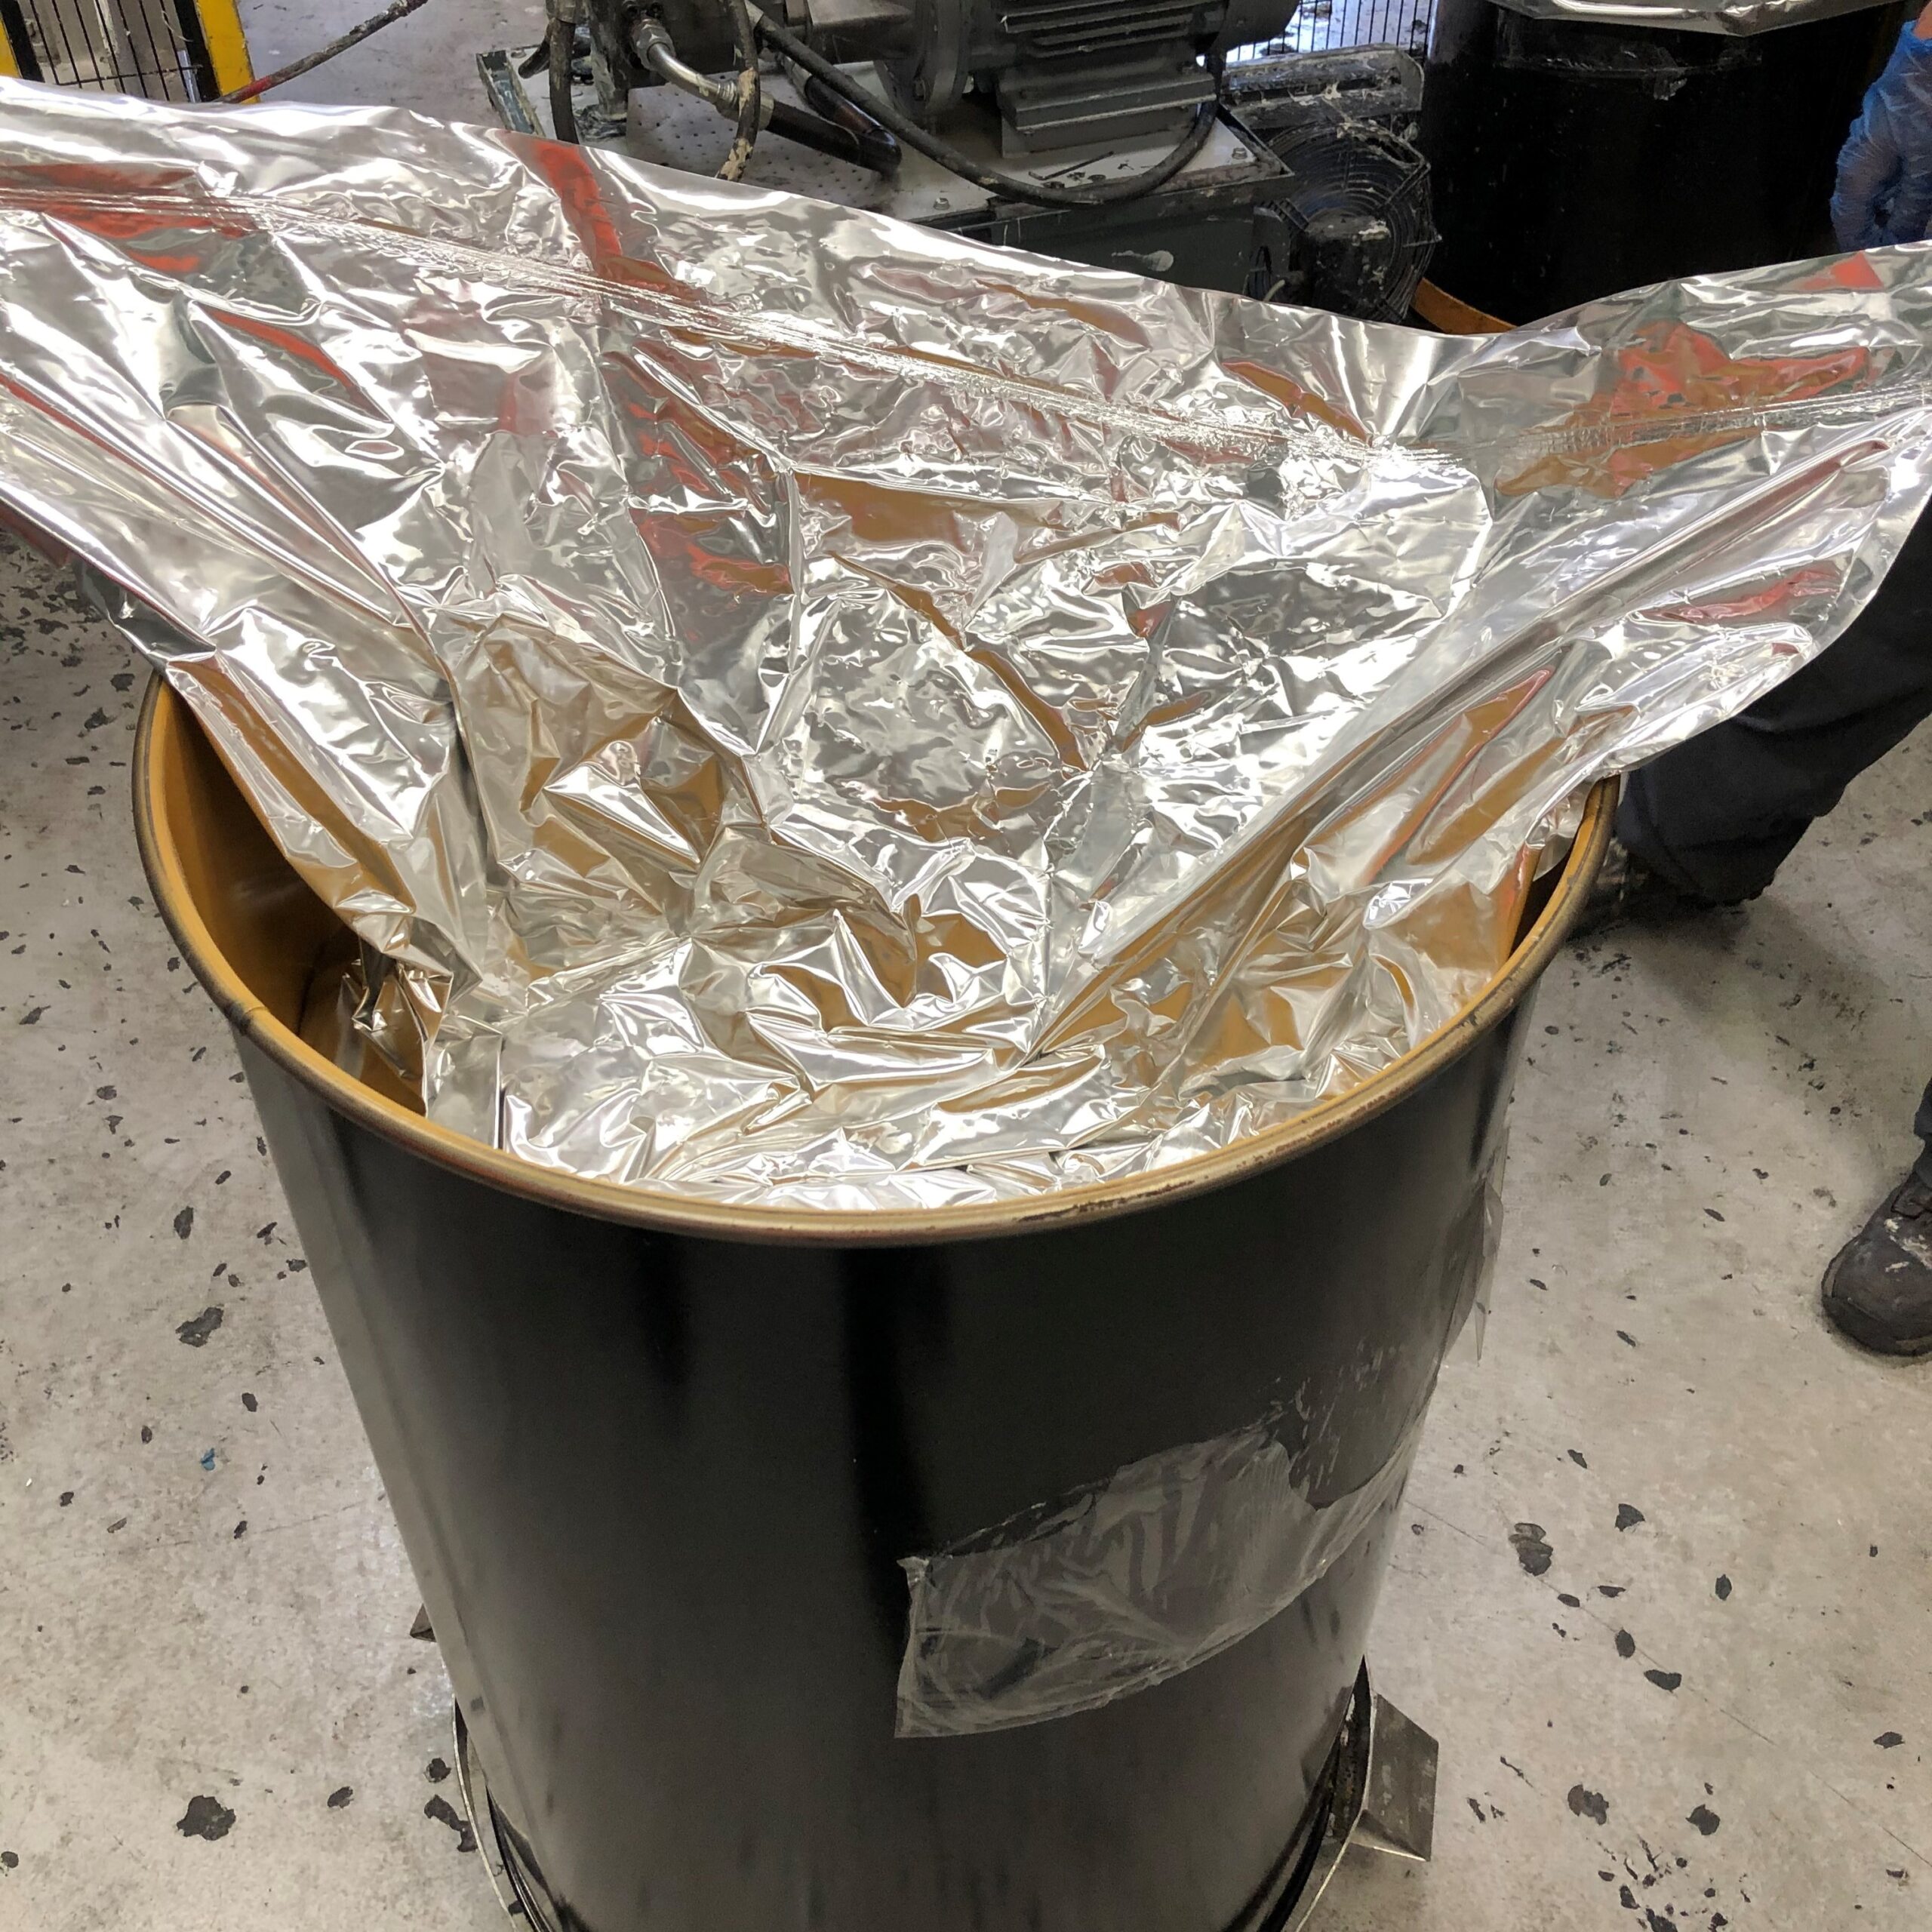
Hazardous & Reactive Materials

Provides a secure, durable barrier against leaks, vapor emissions and unwanted reactions, maintaining safety and stability.
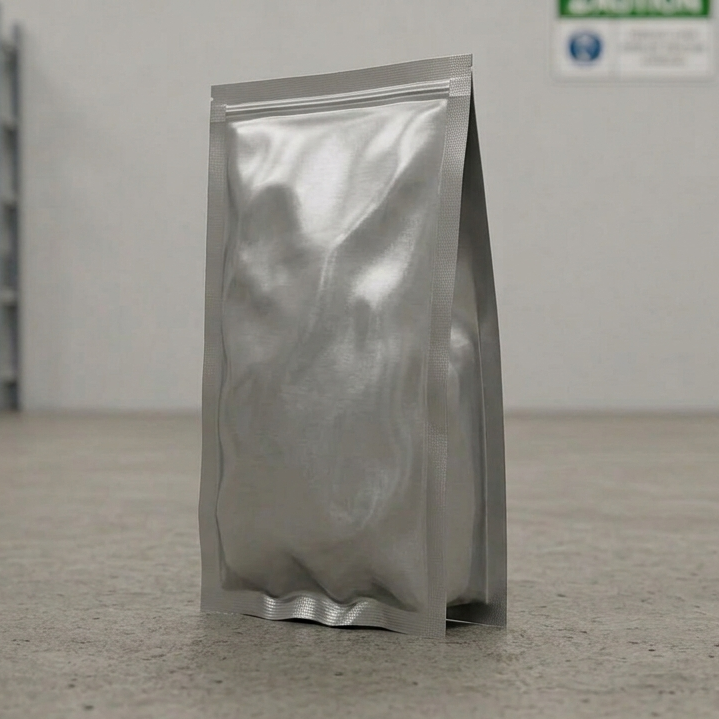
Catalysts, Active Ingredients, & Reagents

Shields sensitive compounds from environmental exposure, preserving efficacy and chemical activity.
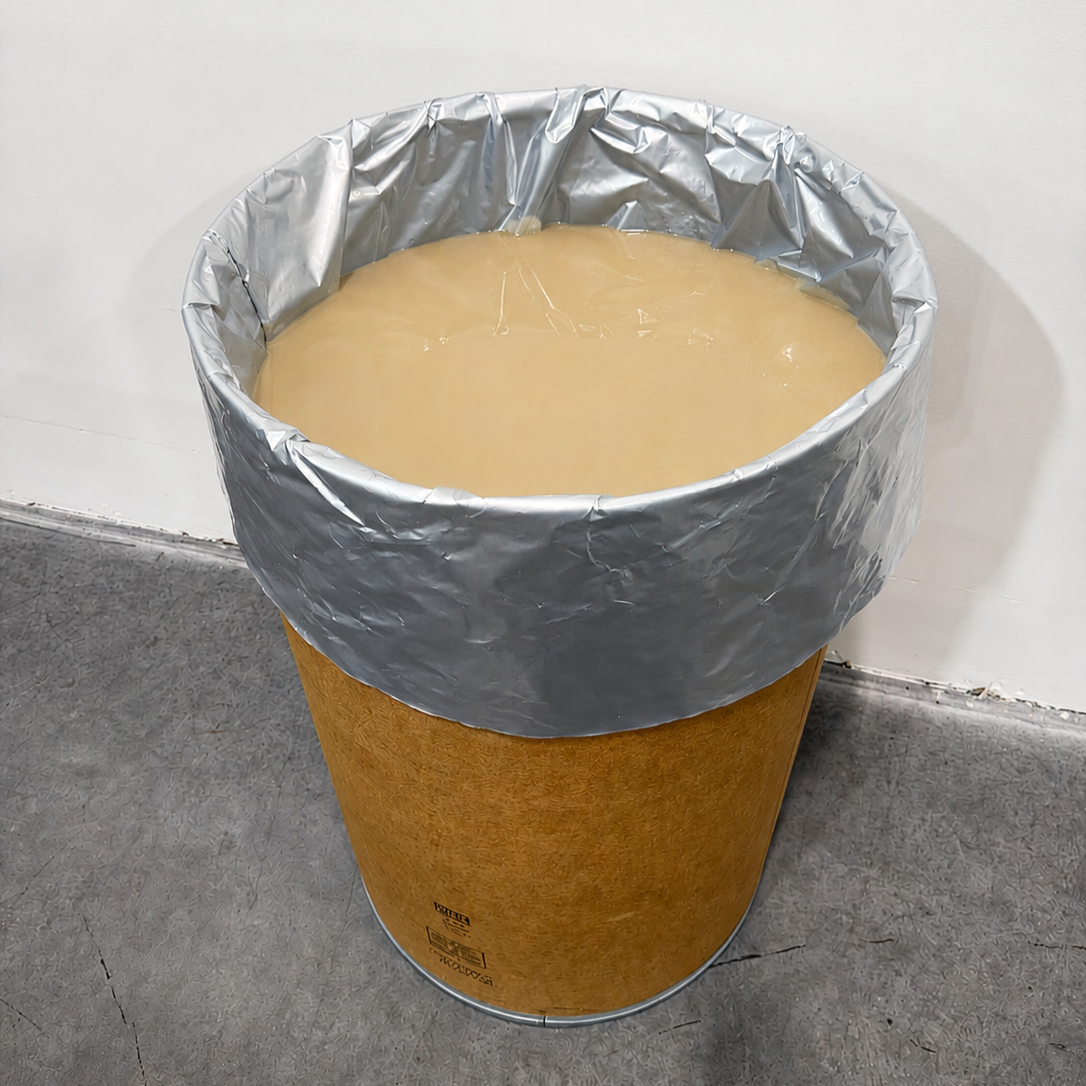
Solvents & Volatile Compounds

Prevents contamination and evaporation, ensuring long-term performance and regulatory compliance.
NO LIMITATIONS ON SIZE, SHAPE OR QUANTITY

Protect Your Products with the Industry’s Most Trusted Barrier Packaging Solution

Contact our expert team today for a customized solution tailored to your specific packaging, storage and transportation needs

FAQ

If you have any further questions or require any further information, please contact us and one of our packaging experts can assist you.

Why is aluminum barrier foil necessary for shipping or storing certain chemicals?

Many chemicals are sensitive to moisture, oxygen and other environmental contaminants that can alter their composition, reduce effectiveness, or shorten shelf life.

Aluminum barrier foil packaging creates a sealed, protective environment that helps preserve product integrity during shipping and storage.

What are the water vapor and oxygen transmission rates of barrier foil packaging?

The Water Vapor Transmission Rate (WVTR) of our barrier foil is <0.0005 g/100inches²/24hrs and the Oxygen Transmission Rate (OTR) is <0.00006 g/100inches²/24hrs. These are the lowest rates of any known flexible material.

These measurements were confirmed by ASTM F 1249 and ASTM D 3985 testing.

Is barrier foil packaging compatible with different types of chemicals?

Yes. Aluminum barrier foil packaging is suitable for a wide range of chemicals, including moisture-sensitive powders, specialty chemicals, intermediates and other industrial materials.

We work directly with you to select the appropriate packaging construction based on your chemical's properties and storage requirements.

What sizes and formats do you offer for packaging chemicals?

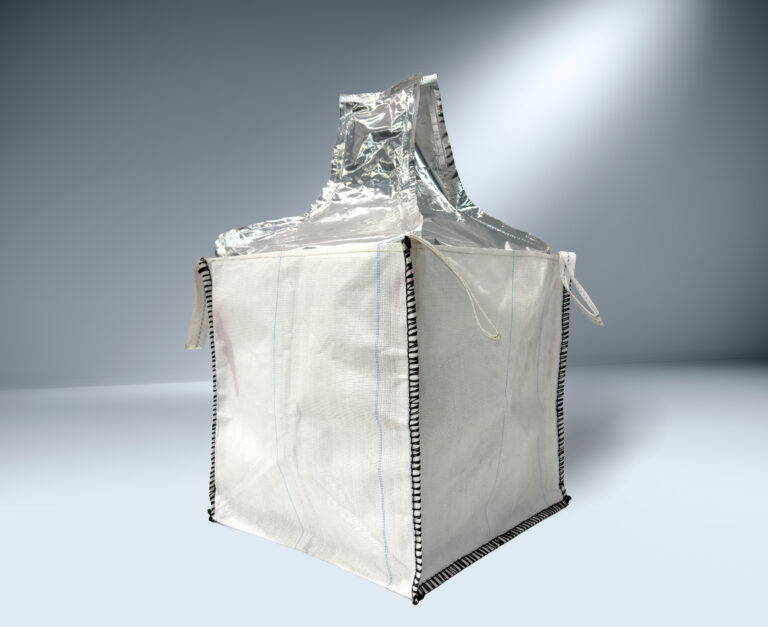
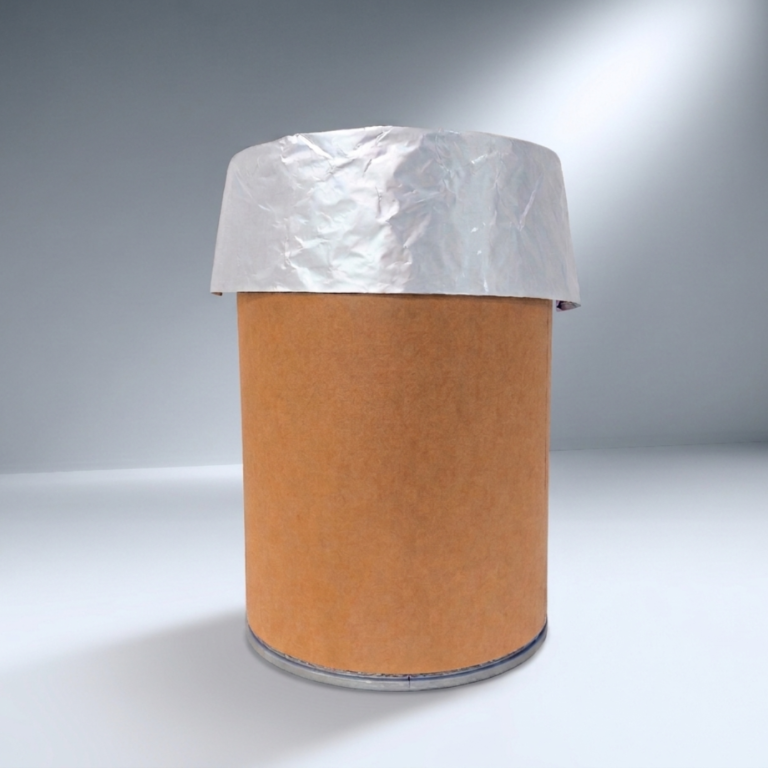
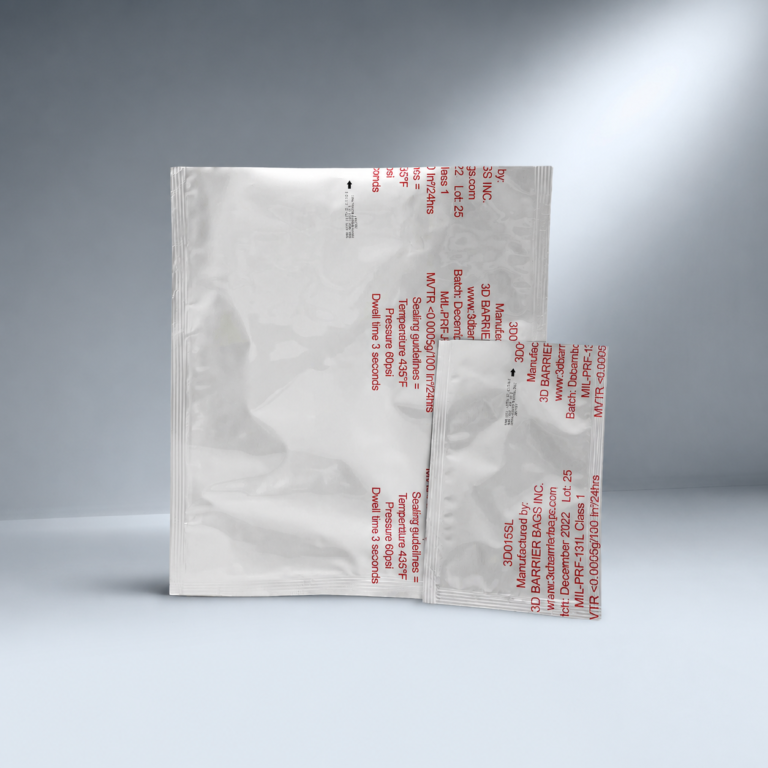
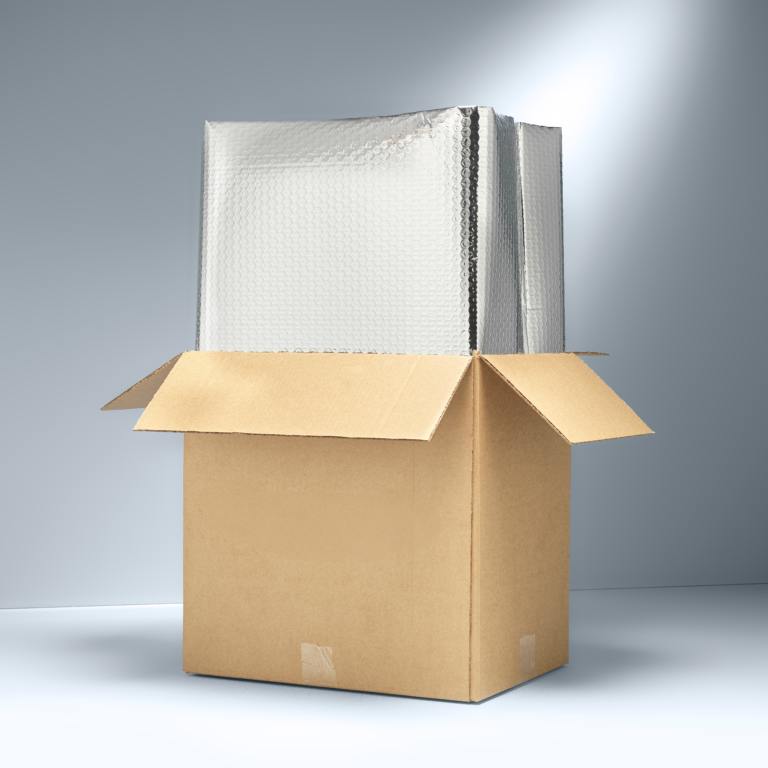
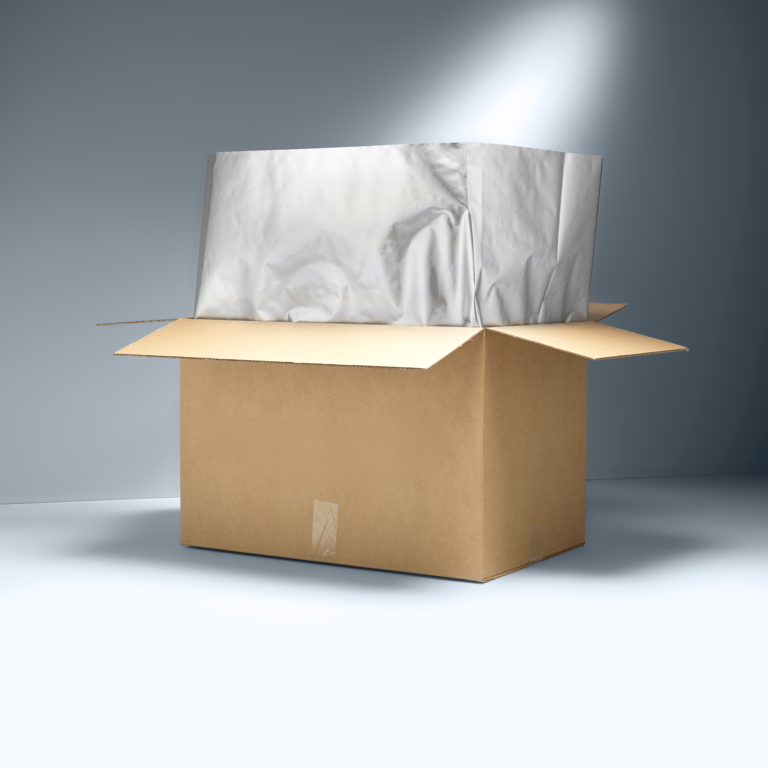
We can convert our barrier foil material into bags and liners of virtually any size or configuration, and we offer multiple formats including Gaylord liners, drum liners, FIBC liners, 55lb. sacks and more.

Is barrier foil packaging suitable for shipping or storing hazardous chemicals?

Barrier foil packaging can be used for certain hazardous chemicals when it is compatible with the product and meets the applicable packaging and transportation regulations.

Because requirements vary by chemical classification, we can assist you in evaluating your specific application and selecting the best packaging solution.

Will barrier foil packaging react with or contaminate my chemicals in any way?

When the appropriate barrier material is selected, the packaging is designed to protect the contents without introducing contaminants or affecting product quality.

We will work with you to recommend the best material and packaging format based on your chemical's compatibility and performance requirements.

HOW OUR QUALITY EXCEEDS INDUSTRY STANDARDS

With stricter regulations and higher quality standards in the chemical industry, safeguarding products from environmental risks is more crucial than ever.
Our aluminum barrier foil bags are certified to military, anti-static and FDA food contact standards, ensuring exceptional protection for sensitive and hazardous materials. Offering the lowest known moisture vapor transmission rate (MVTR) of any flexible packaging material, they:

  • Eliminate the need for modified atmosphere storage and transport, simplifying logistics and reducing costs.
  • Provide consistent, long-term protection against moisture, oxygen, and contaminants.
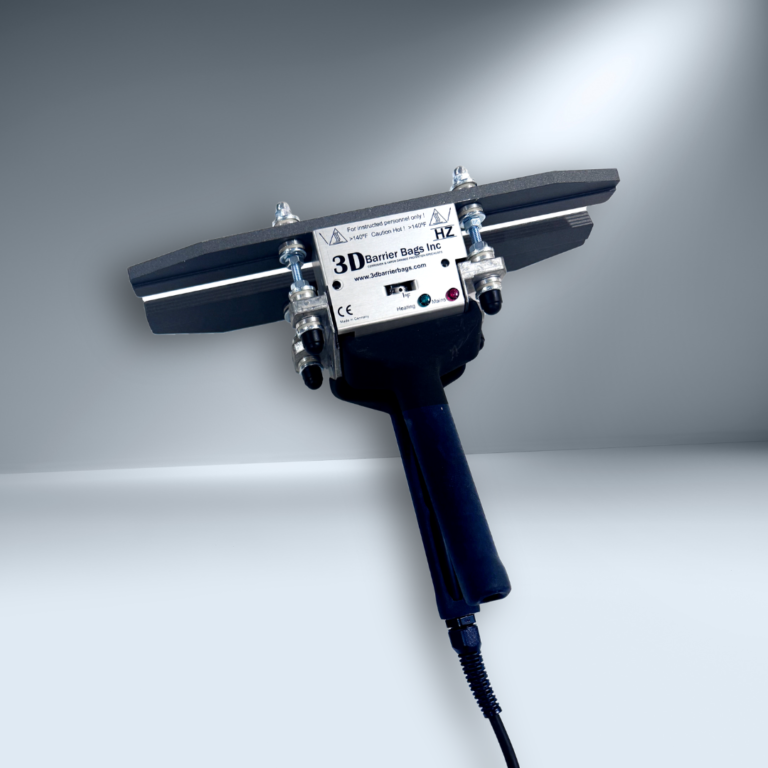
  • Are fully compatible with all end-of-line sealing processes, including gas flushing and vacuum sealing, ensuring a secure, airtight barrier.

Designed to maintain chemical integrity, stability and performance, our aluminum barrier foil bags guarantee optimal protection throughout storage, shipping and handling.

Why Buy From Us

Rapid 24-Hour Turnaround

Industry leading reliability and on-time delivery, without compromising on quality. When you need your products, we’ll make sure they arrive as promised.
No Minimum Order Quantity

We’re here to support your needs.
Order what you want, when you need it.

Dedicated Customer Support

Our expert consultants will find you the right solution, and our dedicated customer support team is here to guide you every step of the way.

Related Information

get in touch

"*" indicates required fields

Brochure Download

Fill out the form below, and you will be redirected to download our brochure.